Brine Filtration Unit Applications in Chemical Processing
Brine Filtration Units are indispensable in chemical processing, ensuring the purity and reliability of brine streams that underpin critical operations such as chlor-alkali production, salt refining, pharmaceuticals, and high salinity wastewater treatment. KES Separation Machinery Co. Ltd (KESMI) is a leading Chinese manufacturer offering advanced, customizable brine filtration solutions designed for both technical excellence and operational efficiency. KESMI units deliver benefits such as contaminant removal, minimized downtime, reduced chemical and maintenance costs, and easy integration with clarification equipment and high salinity wastewater treatment processes.
For professional buyers, KESMI provides tailored engineering, pilot testing, performance guarantees, and support for global compliance needs. Key features include multi-stage filtration, robust corrosion-resistant design, automation, and scalable configurations. With a proven track record in projects worldwide, KESMI stands as a trusted partner for procurement and technical teams seeking high-performance brine filtration equipment that meets the latest industry regulations and business objectives. Contact KESMI for expert consultation and a solution that enhances process reliability, compliance, and profitability.
Introduction: Brine Filtration Units in the Chemical Processing Industry
Brine Filtration Units are critical in the chemical processing industry, securing consistency, reliability, and product purity across a wide array of operations. As a leading manufacturer, KES Separation Machinery Co. Ltd (KESMI) delivers advanced brine filtration equipment designed to exceed the demanding requirements of modern chemical producers. This article explores the distinct applications, advantages, and technical considerations of Brine Filtration Units, including integration with high salinity wastewater treatment and clarification equipment, to strategically support purchasing decisions for plant managers, engineers, and technical procurement specialists.
Core Product Keywords Integrated by KESMI
- Brine Filtration Unit
- High salinity wastewater treatment
- Chemical brine purification system
- Filtration system for chemical processing
- Industrial brine treatment equipment
- Brine clarification units
- Saltwater filtration solution
- Desalination pre-filtration
- Caustic brine filtration
- Chlor-alkali brine purification
- Electrolysis brine filter
- Ion exchange brine pre-treatment
- Brine polishing filter
- Multi-stage brine filtration
- Automatic brine filter skid
- Continuous brine filtration line
Understanding Brine Filtration Unit Technology
At the heart of chemical process optimization lies the Brine Filtration Unit. KESMI’s units are engineered to remove suspended solids, heavy metals, oil, and colloidal particles from brine streams. These impurities, if left unchecked, cause scaling, fouling, and catalyst poisoning in downstream processes such as electrolysis, ion exchange, and specialty chemical synthesis. Our Brine Filtration Units are customizable, available in modular, automatic, and continuous operation designs, and can be seamlessly integrated with clarification equipment or high salinity wastewater treatment trains.
Key Applications of Brine Filtration Units in Chemical Processing
- Chlor-alkali Industry: Ensuring feed brine purity for membrane and diaphragm cells.
- Salt Manufacturing: Removing insoluble contaminants for high-grade salt production.
- Ion Exchange Plants: Pre-treatment of brine before resin columns.
- Electrolysis Units: Maximizing anode/cathode life and product yield by preventing blockages.
- Industrial Wastewater Treatment: Integrated in high salinity wastewater treatment for effective pollutant removal and regulatory compliance.
- Pharmaceuticals and Fine Chemicals: Used in synthesis and separation steps involving brine streams.
- Oil & Gas Operations: Brine filtration for produced water management and enhanced oil recovery.
KESMI’s expertise ensures that each application is addressed with tailored brine filtration solutions to reduce downtime, extend equipment life, and optimize OPEX/CAPEX balance.
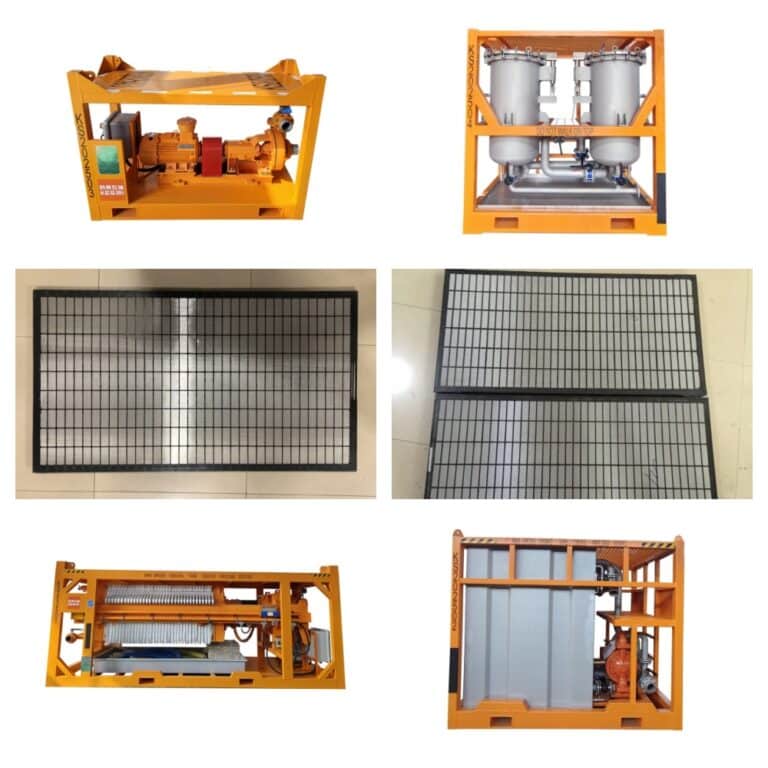
Dual Pod Filtration Unit
Fluids Transfer Pump
Why Choose KESMI Brine Filtration Units?
Purchasing professionals and technical managers face the twin challenge of meeting strict regulatory limits while controlling operational costs. KESMI’s brine filtration technology delivers the following buyer-focused advantages:
- Custom Engineering: Our technical team works closely with clients in chemical processing to analyze brine characteristics, recommend optimal filtration media, and design units that fit seamlessly into existing plants.
- Performance Guarantees: We offer pilot testing, process simulation, and guaranteed contaminant removal rates—crucial for chemical buyers concerned about process reliability.
- Low Maintenance Costs: KESMI’s automatic brine filter skids minimize labor and downtime thanks to robust backwashing and self-cleaning features.
- Global Compliance: Units are delivered with full documentation, supporting buyers’ needs for regulatory certification and plant safety reviews worldwide.
- Fast Delivery and Service: As a direct Chinese manufacturer, KESMI supports rapid project schedules with efficient logistics and responsive after-sales technical support.
Technical Features and Innovations in Brine Filtration Units
- Multi-Stage Filtration: Layered media or cartridge configurations enable removal of particles down to microns or sub-micron sizes, addressing both coarse and fine contaminants.
- Corrosion-Resistant Construction: Units are fabricated from high-grade SS316L, Duplex, or FRP for long service life in corrosive brine environments.
- Automation & Remote Monitoring: Integration with SCADA/DCS systems for real-time monitoring and control, suitable for 24/7 chemical plant operations.
- Energy Efficiency: Optimized hydraulic design reduces pressure drops and power requirements.
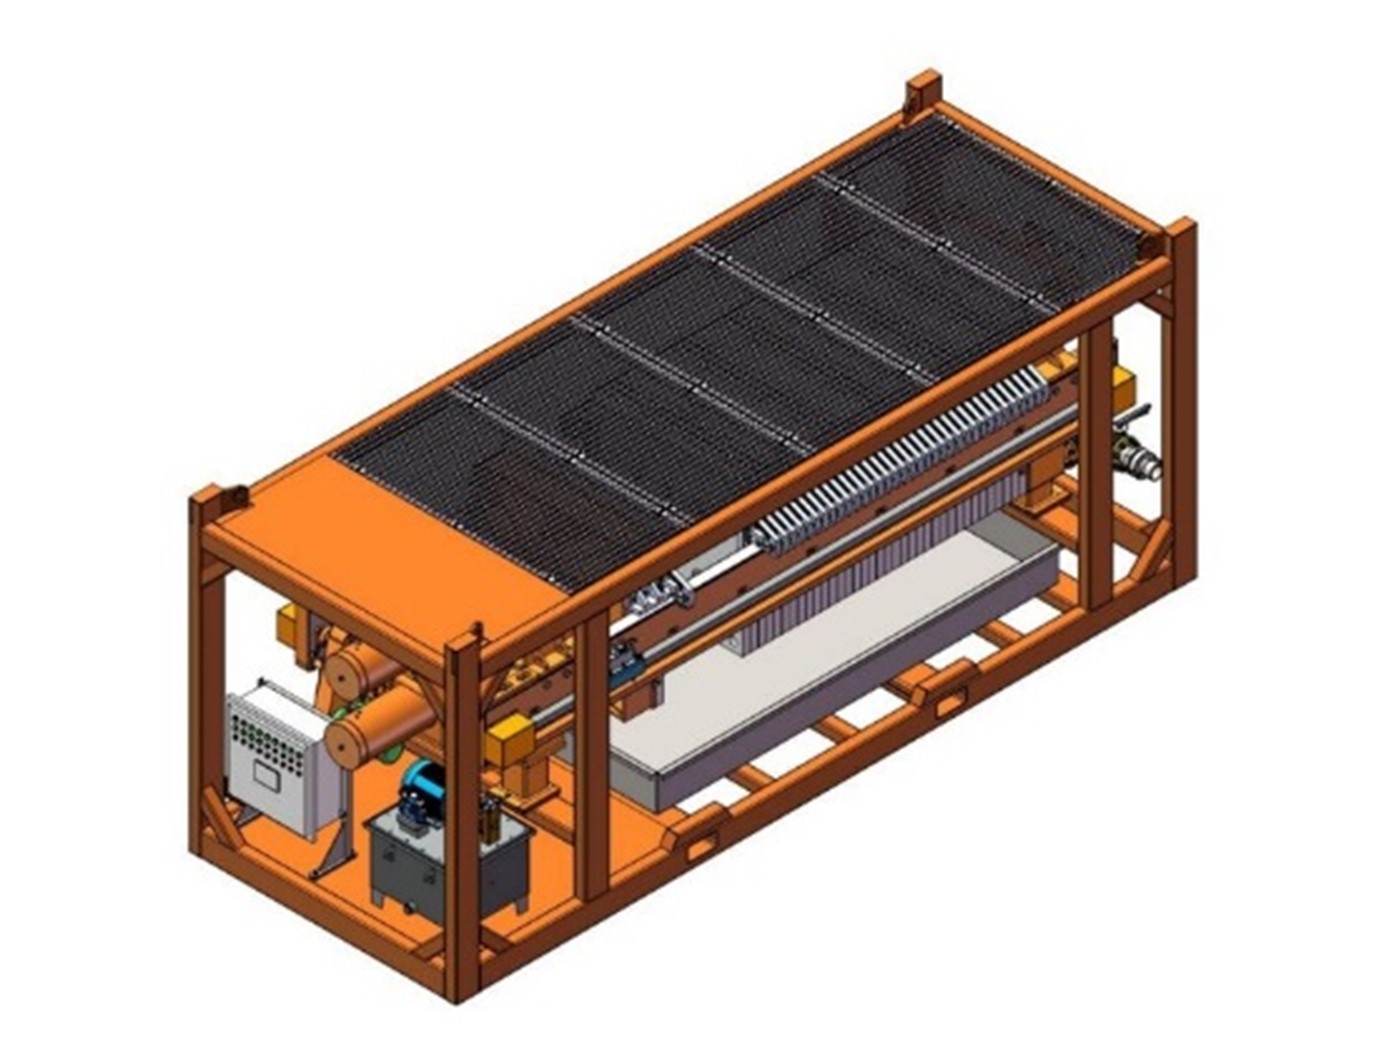
- Modular Scalability: Units are offered as skids or containerized systems, allowing for future capacity expansion and easy plant integration.
KESMI’s engineering team continuously innovates, drawing on global project experience and customer feedback to create brine filtration solutions that set new benchmarks in reliability and performance.
Integration with Clarification Equipment and High Salinity Wastewater Treatment
In many chemical plants, brine filtration units are strategically paired with clarification equipment. Clarification pre-treats brine, removing bulk solids and reducing the load on fine filtration stages. KESMI supplies complete packaged systems, including lamella clarifiers, dissolved air flotation units, and multi-media filters, seamlessly integrated with brine filtration skids.
Moreover, for clients dealing with high salinity wastewater, KESMI’s solutions achieve pollutant removal and TDS reduction targets, supporting discharge and zero liquid discharge (ZLD) mandates. Our technical team can design brine filtration as part of broader high salinity wastewater treatment trains, maximizing water reuse and minimizing sludge generation for chemical plants seeking best-in-class environmental compliance and cost savings.

Competitive Advantages for Chemical Process Buyers
- Maximized Uptime: Robust design and redundancy options ensure continuous operation, vital for buyers prioritizing ROI and production targets.
- Reduced Chemical Consumption: Superior solid-liquid separation decreases coagulant/flocculant demand in downstream stages, directly impacting OPEX.
- Guaranteed Filtrate Quality: Buyers receive documentation and validation data supporting high purity brine for sensitive process steps, such as catalyst beds or pharmaceutical synthesis.
- Flexible Sourcing Options: KESMI offers FOB, CIF, and turnkey project delivery for global buyers, with multi-language support and remote FAT/SAT.
Case Studies: KESMI Brine Filtration Units in Action
- Chlor-Alkali Plant (Asia): KESMI’s multi-stage brine filtration system increased membrane cell lifespan by 30%, cutting brine pre-treatment chemical costs by 18%.
- Specialty Salt Production (Middle East): Automatic brine filtration skid delivered consistent high-purity salt, supporting product certification and export market expansion.
- Pharmaceuticals Manufacturing (Europe): Integrated brine clarification and filtration line met stringent EU GMP standards, with remote monitoring and service support from KESMI engineers.
- Chemical Wastewater Facility (China): High salinity wastewater treatment including brine filtration enabled compliance with new discharge limits and significant reduction in sludge disposal costs.
Deep Dive for Professional Buyers: What to Specify
Experienced technical and procurement professionals know that detail matters when specifying brine filtration units. KESMI’s engineers support buyers with:
- Feed Brine Analysis: Particle load, TDS, oil/grease, heavy metal concentrations.
- Flow Rate & Redundancy: Sizing for peak, average, and turndown flows, with N+1 redundancy for critical lines.
- Filtration Fineness: Selection from 100 micron down to 1 micron or less, depending on downstream sensitivity.
- Materials of Construction: Recommendations for brine, caustic, or acidic environments.
- Automation & Control Requirements: Interface with plant DCS/PLC, data logging, and alarm provisions.
- Maintenance & Spares: Local vs. central maintenance, availability of wear parts, and service contracts.
Engaging with KESMI in the early stages of project planning allows procurement teams to obtain process guarantees, optimize TCO, and minimize risk.
Frequently Asked Questions: Brine Filtration Units by KESMI
| Question | Answer |
|---|---|
| What contaminants can KESMI brine filtration units remove? | Suspended solids, silica, algae, oil, heavy metals, and organic matter, depending on selected filtration media and configuration. |
| Can the units operate in harsh chemical environments? | Yes, with materials including SS316L, FRP, and Duplex steel for excellent corrosion resistance. |
| How are brine filtration systems maintained? | Units feature automatic backwash/self-cleaning, with periodic media/cartridge changeouts as required by brine quality and loading. |
| Can KESMI support global projects? | Absolutely. We deliver worldwide with support for export certification, remote FAT, and multi-language documentation. |
| What is the typical delivery time? | Standard units: 8-12 weeks. Custom designs: 12-20 weeks, depending on complexity and project requirements. |
Procurement Guidance: How to Partner with KESMI
- Site Visit & Consultation: KESMI engineers can visit your facility or conduct remote assessments to review brine characteristics and process needs.
- Sample Testing: Send brine samples for pilot testing in our laboratories, receiving detailed performance reports and process recommendations.
- Proposal & Quotation: Receive transparent quotations with clear technical and commercial terms, including guaranteed filtration performance and after-sales service packages.
- Project Execution: Dedicated project managers oversee production, testing, delivery, and supervision of installation/commissioning as required.
- Long-Term Partnership: Buyers benefit from ongoing technical support, spare parts supply, and upgrade/expansion options as operations grow.

Conclusion: Invest in KESMI Brine Filtration Units for Sustainable Chemical Processing
For procurement professionals and technical managers in the chemical industry, the right brine filtration unit is an investment in product quality, plant uptime, and regulatory compliance. With a proven track record and a commitment to customer-centric engineering, KES Separation Machinery Co. Ltd (KESMI) stands as the trusted choice for industrial brine treatment equipment worldwide. Our broad product portfolio covers every aspect of brine purification, from high salinity wastewater treatment integration to advanced clarification equipment, all backed by responsive after-sales support and a focus on driving long-term value for chemical buyers.
If your chemical process line requires reliable brine filtration, or if you seek to upgrade existing systems for higher efficiency and lower operating costs, partner with KESMI for a tailored solution. Contact us today to discuss your project needs and discover how our technology can safeguard your operations, support compliance, and enhance overall profitability.
Contact KES Separation Machinery Co. Ltd (KESMI)
For quotations, technical inquiries, or to arrange a site visit, contact our global sales and engineering team via www.kes-separation.com or email [email protected]. Our professionals are ready to support your brine filtration unit project from initial concept to operational excellence.