Brine Filtration Equipment for Sustainable Resource Recovery
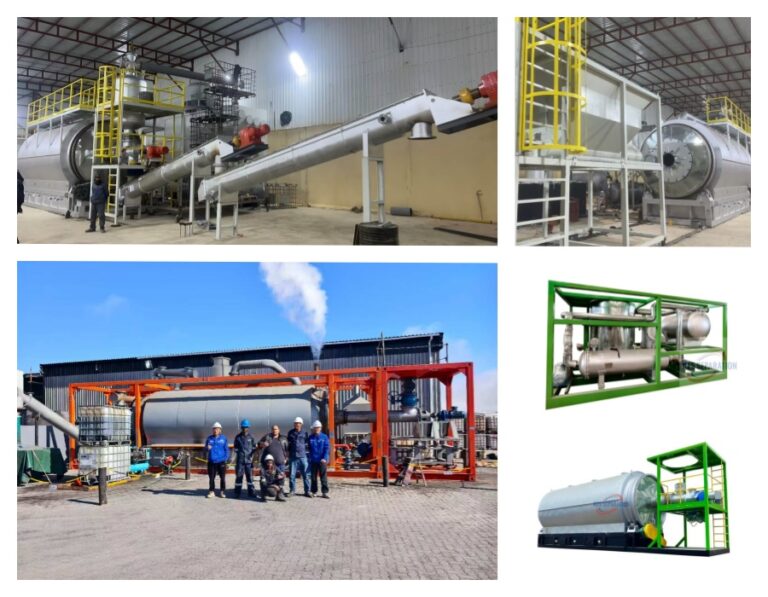
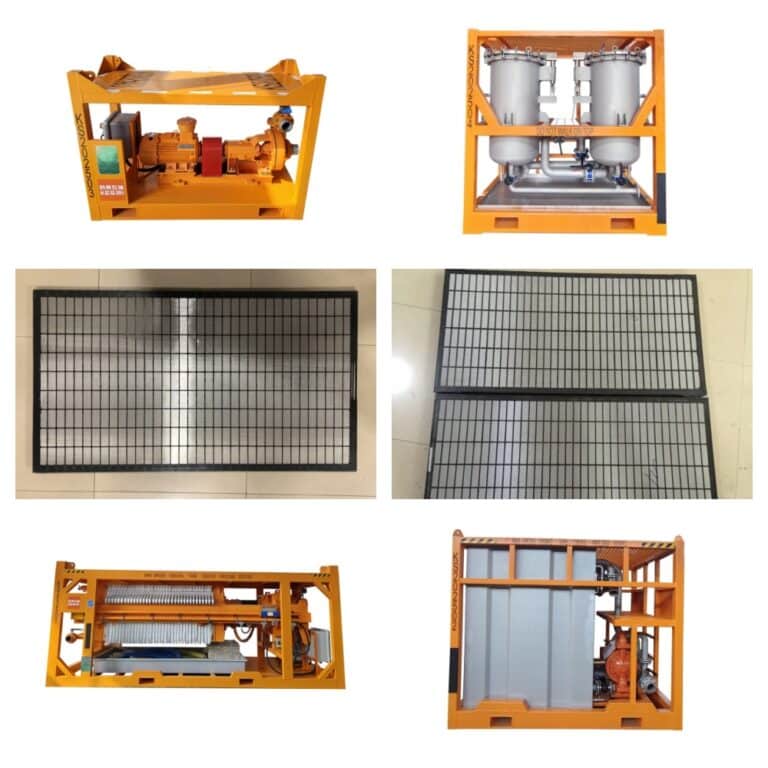
KES Separation Machinery Co. Ltd (KESMI) offers advanced brine filtration equipment designed for sustainable resource recovery. Integrating key technologies such as brine filtration systems, membrane filtration, salt recovery, industrial wastewater treatment, zero liquid discharge (ZLD), and desalination pre-treatment, KESMI provides scalable, efficient, and customizable solutions for industrial buyers. The company’s technical expertise ensures high-efficiency filtration, multi-stage purity, automatic operation, and reliable performance in harsh environments, directly addressing procurement priorities like operational uptime, cost savings, and environmental compliance. KESMI’s proven track record in global deployments and after-sales support, combined with ISO certification and flexible customization, makes it the preferred choice for genuine purchasers seeking future-ready, sustainable resource recovery systems. Real-world case studies highlight significant cost reductions, enhanced productivity, and regulatory compliance achieved through KESMI’s solutions. Buyers are encouraged to engage with KESMI for technical consultations and tailored quotations to ensure maximum ROI and operational excellence.
Brine Filtration Equipment for Sustainable Resource Recovery: The KESMI Advantage
Introduction to Brine Filtration Equipment and Sustainable Solutions
Buyers seeking advanced brine filtration equipment for sustainable resource recovery often face challenges related to efficiency, scalability, and reliability. As a leading Chinese manufacturer, KES Separation Machinery Co. Ltd (KESMI) has developed solutions tailored to industrial needs, providing robust and innovative technologies that address both environmental and economic demands. Integrating product keywords such as brine filtration system, membrane filtration, salt recovery, industrial wastewater treatment, zero liquid discharge (ZLD), desalination pre-treatment, high-efficiency filtration, multi-stage filtration, automatic filter units, resource recovery, corrosion-resistant filtration, chemical filtration, modular filtration equipment, membrane filtration units, pressure filtration systems, backwash filtration, brine treatment plant, customized filtration solutions, and continuous filtration systems, KESMI enables buyers to achieve sustainable operations and maximize returns.
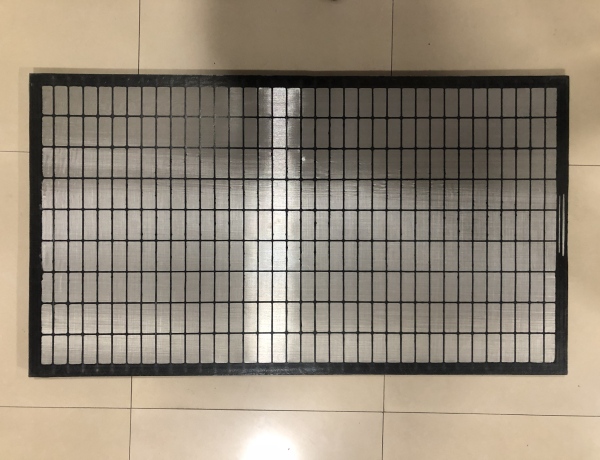
Deep Understanding of Buyer Needs: Procurement Perspective
Experienced procurement personnel prioritize not only product quality but also after-sales service, scalability, and compliance with environmental regulations. KESMI’s brine filtration equipment is designed with these priorities in mind. From modular filtration equipment to customized filtration solutions, we offer a range of brine treatment plant options that address unique industrial needs and ensure future-ready investments. Our automatic filter units and continuous filtration systems minimize operational downtime, boosting productivity and profitability for buyers.
Technical Excellence: Professional Perspective
KESMI’s technical team leverages decades of experience in membrane filtration and pressure filtration systems to deliver unparalleled performance. Our multi-stage filtration units enable precise salt recovery and resource recovery, ensuring that industrial wastewater treatment meets stringent regulations. Corrosion-resistant filtration and chemical filtration modules are engineered for reliability, even in the harshest environments. For buyers seeking zero liquid discharge (ZLD) capabilities, our backwash filtration and desalination pre-treatment technologies provide the foundation for sustainable resource recovery and environmental compliance.
Product Keywords Integrated Into KESMI Brine Filtration Solutions
- brine filtration system: Robust, scalable, and efficient solutions for industrial brine treatment.
- Membrane Filtration: Advanced membrane technology for optimal separation and purification.
- Salt Recovery: Integrated modules for high-yield salt extraction and reuse.
- Industrial Wastewater Treatment: Comprehensive systems addressing both liquid and solid waste streams.
- Zero Liquid Discharge (ZLD): Complete solutions for minimizing environmental impact.
- Desalination Pre-Treatment: Pre-filtration systems for seawater and brine desalination processes.
- High-Efficiency Filtration: Optimized units delivering maximum throughput with energy savings.
- Multi-Stage Filtration: Sequential filtration modules for enhanced purity and recovery.
- Automatic Filter Units: Smart, automated filtration for reduced maintenance and labor costs.
- Resource Recovery: Technology focusing on valuable by-product extraction from brine streams.
- Corrosion-Resistant Filtration: Engineered to withstand aggressive chemical environments.
- Chemical Filtration: Precision systems for selective removal of contaminants.
- Modular Filtration Equipment: Flexible configurations for changing operational demands.
- Membrane Filtration Units: Specialized modules for ultra-fine separation tasks.
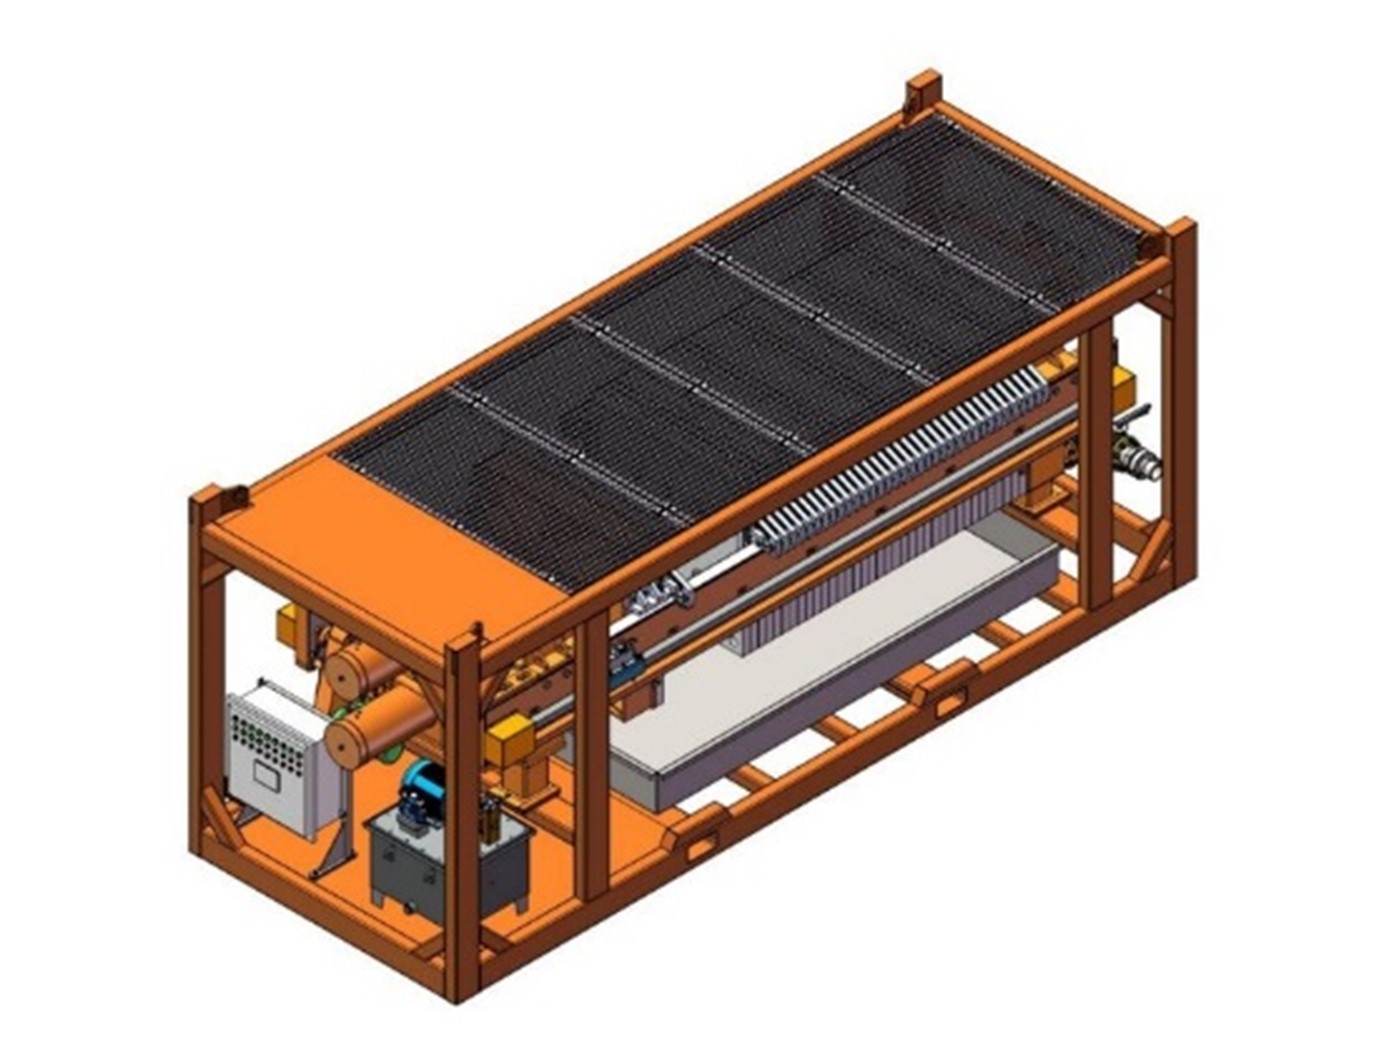
- Pressure Filtration Systems: High-pressure units for demanding industrial applications.
- Backwash Filtration: Self-cleaning technology to maintain continuous operation.
- Brine Treatment Plant: Complete, turnkey solutions for industrial-scale brine management.
- Customized Filtration Solutions: Tailored systems according to buyer-specific requirements.
- Continuous Filtration Systems: Real-time, uninterrupted filtration for process industries.
Special Keyword Focus: Zero Liquid Discharge (ZLD) and Desalination Pre-Treatment
Zero liquid discharge (ZLD) is an imperative for industries aiming to minimize environmental footprints. KESMI’s ZLD brine filtration equipment integrates multi-stage filtration and backwash filtration, supporting buyers in achieving regulatory compliance and resource efficiency. Our desalination pre-treatment systems are engineered for seawater and highly concentrated brine, ensuring long membrane lifespan, reduced maintenance costs, and high-quality output water for downstream processes. These solutions are proven in power plants, chemical industries, and mining operations where sustainable resource recovery is a key procurement requirement.
Why Choose KESMI: Proven Chinese Manufacturer Credentials
KES Separation Machinery Co. Ltd is recognized for its commitment to quality, innovation, and customer satisfaction. Our brine filtration equipment is backed by ISO certification, rigorous testing protocols, and a dedicated technical support team. Buyers benefit from factory-direct pricing, fast delivery, and flexible customization options. Case studies demonstrate successful deployments in Asia, Europe, and the Americas, showcasing our international reach and reliability.
Buyer Benefits: Maximizing ROI and Operational Efficiency
- Cost Savings: High-efficiency filtration reduces energy and chemical consumption.
- Sustainability: ZLD and resource recovery ensure compliance and reduce waste.
- Productivity: Automatic filter units and continuous filtration systems enhance process uptime.
- Customization: Modular and tailored solutions address evolving industrial requirements.
- Support: Professional after-sales service and global technical support.
Technical Specifications and Customization Options
| Product Keyword | Specification | Industrial Application |
|---|---|---|
| Brine Filtration System | Flow rates 10–1000 m3/h; corrosion-resistant materials | Salt production, chemical processing |
| Membrane Filtration | UF, NF, RO modules; pore size 0.01–0.1 micron | Water purification, ZLD process |
| Salt Recovery | Crystallizer integration; automated discharge | Food-grade salt, industrial reuse |
| Industrial Wastewater Treatment | Multi-stage filtration; PLC control | Mining, oil & gas, manufacturing |
| Automatic Filter Units | Backwash cycles; sensor monitoring | Continuous operation plants |
| Desalination Pre-Treatment | Antiscalant dosing; high-pressure pumps | Seawater desalination |
Case Studies: Real Buyer Successes
One client in the chemical industry adopted KESMI’s pressure filtration systems and achieved a 30% reduction in brine waste, leading to substantial cost savings. In a mining operation, modular filtration equipment enabled rapid scaling as production demands increased. Our ZLD solutions facilitated regulatory compliance in a power generation facility, eliminating liquid discharge and enabling resource recovery. These real-world examples demonstrate KESMI’s ability to deliver on both technical and commercial requirements.
Global Reach and Professional Support
KESMI’s brine treatment plants and customized filtration solutions are deployed worldwide, supported by multilingual technical teams. Buyers receive comprehensive documentation, training, and remote monitoring services to ensure optimal system performance. We understand procurement complexities and deliver factory-direct solutions that streamline sourcing processes and minimize risk.
Future-Ready Sustainability: Meeting Evolving Challenges
As environmental regulations tighten and resource scarcity increases, KESMI’s brine filtration equipment stands out as a future-ready investment. Whether targeting high-efficiency filtration or specialized membrane filtration units for advanced applications, buyers can rely on us for innovative, durable, and scalable solutions that support sustainable industrial growth.

Conclusion: Contact KESMI for Genuine Purchasing Solutions
For buyers seeking reliable, high-performance brine filtration equipment for sustainable resource recovery, KES Separation Machinery Co. Ltd (KESMI) is the proven partner. Our expertise, product range, and commitment to customer success make us the preferred choice for industrial-scale filtration. Contact our procurement team for technical consultations, quotations, and tailored solutions designed to maximize your operational returns and achieve environmental excellence.
References and Further Reading
- ISO Certified Brine Filtration Equipment – Quality Assurance Documentation
- Case Studies in Salt Recovery and ZLD – KESMI Technical Reports
- Resource Recovery Technologies – Industry White Papers
- Industrial Wastewater Treatment Guidelines – Regulatory Compliance Resources