What Makes a Thermal Desorption System Ideal for Waste Treatment
KES Separation Machinery Co. Ltd (KESMI) offers advanced thermal desorption systems ideal for waste treatment, with a focus on contaminated soil remediation, hazardous waste management, and industrial sludge processing. This article explains how KESMI’s solutions cater to buyers seeking high-performance, scalable, and compliance-driven machinery. Integrated with key technologies like soil washing plant and pyrolysis reactor, KESMI thermal desorption systems efficiently recover hydrocarbons, control VOC emissions, and remove heavy metals, assuring environmental compliance and operational cost savings. The article addresses procurement psychology, highlighting KESMI’s robust after-sales support, global service network, and technical transparency—all factors critical for genuine buyers. Case studies demonstrate proven success in industrial scale remediation, and a procurement guide assists buyers in selecting the right equipment for their needs. As a leading Chinese manufacturer, KESMI combines innovation, reliability, and value, making it the preferred partner for waste treatment projects worldwide.
Introduction to Thermal Desorption System for Waste Treatment
As global environmental regulations tighten and industries strive for sustainable risk management, the demand for advanced waste treatment solutions is surging. At KES Separation Machinery Co. Ltd (KESMI), we specialize in thermal desorption systems designed to address the complexities of contaminated soil remediation, hazardous waste destruction, and industrial sludges. This article draws from the perspective of professional technical personnel and experienced procurement specialists, seeking to provide genuine buyers with deep insights into thermal desorption technology and its optimal application in modern waste management.
Key Product Keywords Integrated in Waste Treatment Solutions
- Thermal desorption system
- Contaminated soil remediation
- Hazardous waste treatment
- Sludge treatment equipment
- Industrial waste remediation
- Hydrocarbon recovery unit
- VOC emission control
- Pyrolysis reactor
- Indirect heating system
- Rotary kiln desorption
- Soil washing plant
- Heavy metals removal
- Waste oil recycling
- Environmental compliance machinery
- Automated process control
- Energy-efficient waste treatment
- Regenerative thermal oxidizer
- Continuous operation system
- Mobile remediation plant
- Industrial scale remediation
Buyer Psychology: Why Choose KESMI Thermal Desorption Systems?
Procurement decisions are driven by a blend of technical confidence, regulatory compliance, ROI, and operational reliability. Buyers seeking a thermal desorption system prioritize proven performance, scalability, and after-sales support. KESMI leverages decades of manufacturing excellence, offering systems tailored for contaminated soil remediation, sludge treatment equipment, and hazardous waste management. Our solutions assure buyers of seamless integration, minimal downtime, and robust automation, catering to the needs of both multinational environmental contractors and municipal authorities.
Technical Advantages of KESMI Thermal Desorption Systems
1. Precision Engineering & High Efficiency
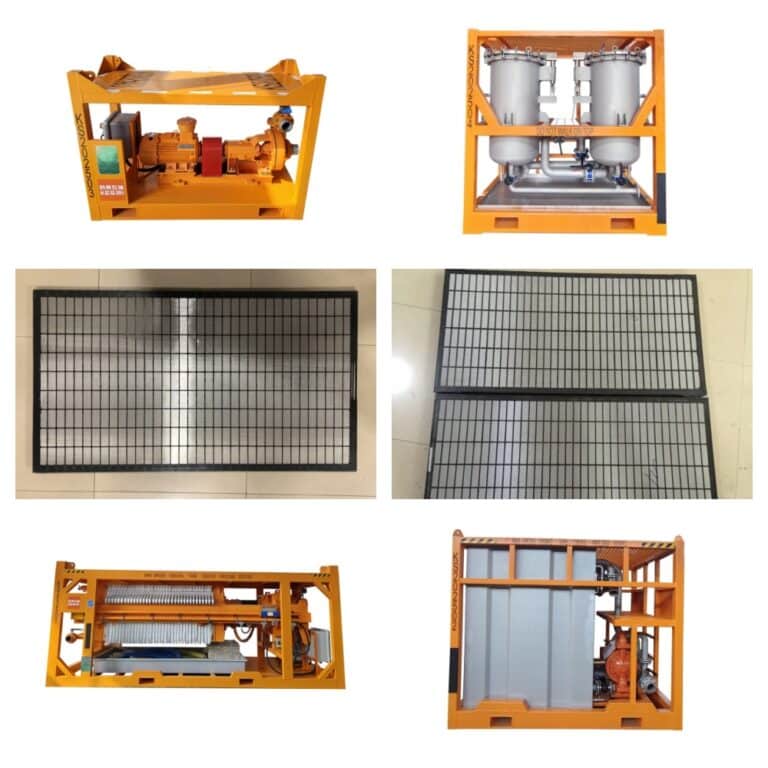
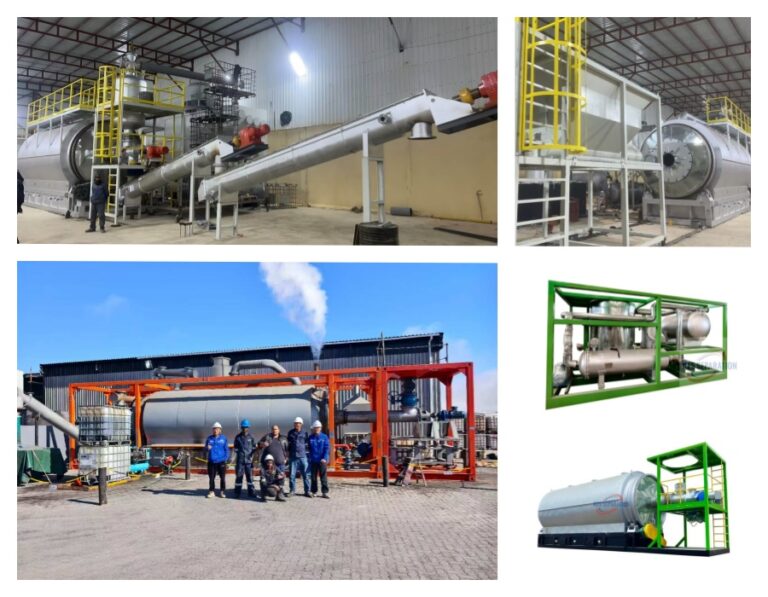
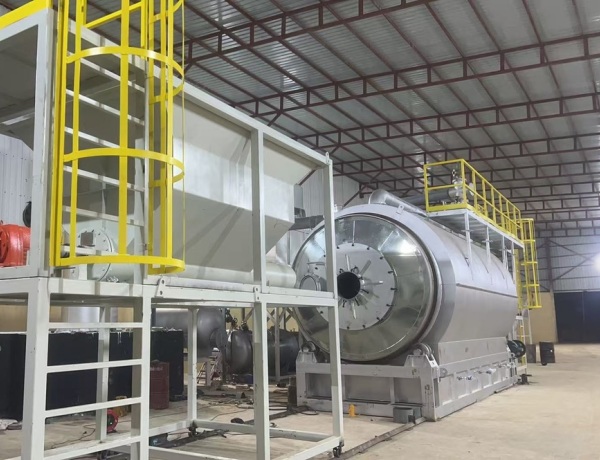
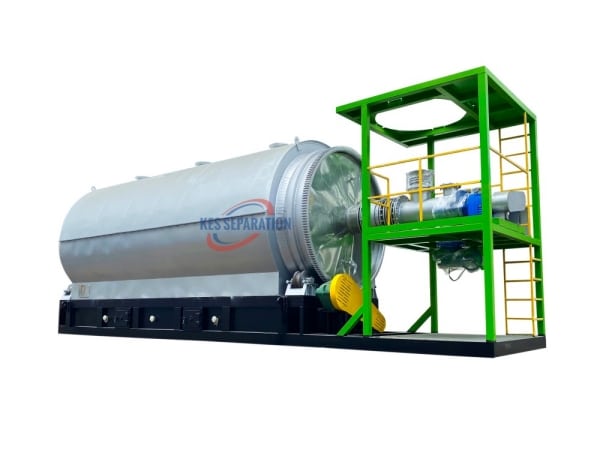
KESMI’s thermal desorption systems incorporate indirect heating system technology for uniform heat distribution, ensuring rapid desorption of hydrocarbons and VOCs from soils and industrial sludges. Our rotary kiln desorption units are engineered for continuous operation, maximizing throughput and minimizing operator intervention—critical for large-scale contaminated soil remediation and industrial waste remediation projects.
2. Versatile Application Range
Our systems are compatible with a wide array of waste streams: from refinery sludges, hazardous chemical spills, and municipal waste oils, to heavy metals removal and hydrocarbon recovery unit operations. KESMI’s mobile remediation plant designs offer flexibility for on-site treatment, reducing logistics costs for buyers and ensuring swift regulatory compliance.
3. Advanced Process Control
Automated process control is central to KESMI’s machinery. Every thermal desorption system features precision sensors, real-time monitoring, and adaptive feedback loops, optimizing energy consumption and ensuring environmental compliance. Regenerative thermal oxidizer technology is integrated to efficiently manage VOC emission control, further aligning with global air quality standards.
KESMI Product Portfolio: Meeting Diverse Waste Treatment Needs
| Product Model | Key Application | Processing Capacity | Special Features |
|---|---|---|---|
| TD-500 Rotary Kiln | Contaminated soil remediation | 500 T/day | Indirect heating, continuous operation |
| TD-MP Mobile Plant | Industrial waste remediation | 100 T/day | Portable, rapid deployment |
| TD-S Hydrocarbon Recovery | Waste oil recycling | 300 T/day | Energy-efficient, VOC control |
| TD-H Heavy Metals Removal | Hazardous waste treatment | 200 T/day | Automated process control |
Integration of Soil Washing Plant and Pyrolysis Reactor Keywords
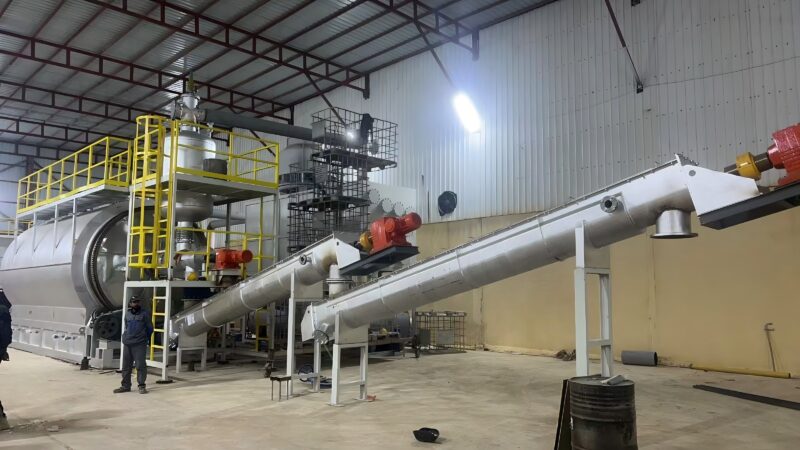
KESMI thermal desorption systems excel when integrated with soil washing plant technology, enabling enhanced separation of mineral fragments and organic contaminants. This synergy amplifies the effectiveness of contaminated soil remediation, especially in complex industrial sites. Additionally, our pyrolysis reactor units offer buyers the capability to convert organic waste into valuable by-products, such as biochar and syngas, adding a lucrative dimension to waste treatment operations.
Environmental Compliance and Cost Efficiency
Our machinery is engineered for environmental compliance machinery standards—meeting China, EU, and US emission benchmarks. Buyers benefit from minimized regulatory risk and reduced fines. Energy-efficient waste treatment means lower utility costs and improved sustainability metrics, vital for procurement specialists targeting ROI and CSR objectives.
After-Sales Support and Global Service Network
KESMI stands out for its comprehensive after-sales support, including remote diagnostics, on-site commissioning, and spare parts logistics. Genuine buyers get access to our global service network, ensuring operational continuity and maximizing asset uptime. Our professional technical personnel are always available for consultation, training, and system optimization.
Case Studies: Proven Results in Industrial Scale Remediation
- Petrochemical Complex (Asia): Deployed TD-500 Rotary Kiln for hydrocarbon recovery and contaminated soil remediation, achieving 96% pollutant removal and full regulatory compliance.
- Municipal Sludge Plant (Europe): Utilized TD-MP Mobile Plant for hazardous waste treatment, reducing operational costs by 30% and streamlining waste logistics.
- Mining Site (Africa): Integrated TD-H Heavy Metals Removal with soil washing plant, enabling efficient separation and safe disposal of heavy metal contaminants.
Procurement Guide: How to Select the Right Thermal Desorption System
- Define waste stream composition: soil, sludge, oil, or mixed industrial waste.
- Determine processing volume: KESMI offers scalable solutions from 50 T/day to 700 T/day.
- Assess regulatory requirements: Our systems are tailored for international compliance.
- Evaluate integration needs: Soil washing plant, pyrolysis reactor, VOC emission control.
- Consider automation and remote monitoring options.
- Request full lifecycle support: Installation, training, maintenance, upgrades.
Why KESMI is the Preferred Chinese Manufacturer for Genuine Buyers
As a Chinese manufacturer with global reach, KESMI combines cost-effective production with cutting-edge technology. Our thermal desorption systems are trusted by government, industry, and environmental service providers worldwide. Buyers benefit from custom engineering, fast delivery, and technical transparency, all backed by robust export logistics and documentation.
Frequently Asked Questions (FAQ)
- What waste streams are compatible with KESMI thermal desorption systems? Soil, sludge, oil, refinery waste, hazardous chemicals.
- How does your system ensure environmental compliance? Integrated VOC emission control, advanced sensors, and real-time monitoring.
- Can KESMI systems be deployed globally? Yes, our machinery is designed for international standards and fast logistics.
Contact KESMI for Genuine Buyer Consultation
If you are a procurement specialist or technical manager seeking proven, high-performance thermal desorption systems for contaminated soil remediation, hazardous waste treatment, sludge treatment equipment, or industrial waste remediation, contact KESMI today. Our professional technical personnel will tailor solutions to your requirements and ensure a seamless buying experience.
Conclusion: The Ideal Solution for Waste Treatment
KESMI’s thermal desorption system portfolio delivers unmatched performance, flexibility, and compliance for buyers focused on genuine waste treatment outcomes. Integrated with soil washing plant and pyrolysis reactor technologies, our systems turn waste into value, ensuring environmental stewardship and operational excellence. Choose KESMI for your next waste remediation project and experience the professionalism and technical depth that only an experienced Chinese manufacturer can offer.
Tags:Thermal Desorption Unit factory,Thermal Desorption Unit Customized,Thermal Desorption Unit,Thermal Desorption Unit supplier