Continuous Thermal Desorption Unit Solutions for Industrial Cleanup
KES Separation Machinery Co. Ltd (KESMI), a leading Chinese manufacturer, specializes in advanced continuous thermal desorption units for industrial cleanup, soil remediation, hazardous waste treatment, and VOCs removal. KESMI’s solutions feature modular design, integrated process automation, real-time monitoring, and robust emission controls, tailored to diverse industrial demands such as contaminated soil treatment and environmental restoration. With a focus on buyer priorities—reliability, compliance, operational efficiency, and long-term cost savings—KESMI delivers not only high-performance machinery but also comprehensive after-sales service, technical consulting, and proven global results. Two keywords, VOCs removal technology and PLC control system, highlight KESMI’s commitment to emission safety and fully automated operation, ensuring buyers achieve regulatory compliance and project certainty. Tested in oil refineries, chemical plants, and land redevelopment, KESMI’s continuous thermal desorption units are trusted by genuine purchasing buyers aiming for operational excellence and sustainable environmental protection. Contact KESMI for expert consulting and tailored industrial cleanup solutions, backed by deep manufacturing expertise and commitment to buyer success.
continuous thermal desorption unit Solutions for Industrial Cleanup – KES Separation Machinery Co. Ltd (KESMI)
Introduction to Continuous Thermal Desorption and KESMI Expertise
Industrial cleanup faces ever-increasing demands for efficiency, reliability, and environmental compliance. At the forefront of this field stands KES Separation Machinery Co. Ltd (KESMI), a leading Chinese manufacturer specializing in the development and delivery of advanced continuous thermal desorption units (CTDU). As a professional procurement or technical expert, you understand that choosing the right thermal desorption system directly impacts operational success, regulatory adherence, and long-term cost efficiency. KESMI’s CTDU solutions are engineered for optimal performance in soil remediation, hazardous waste treatment, and VOCs removal, among other industrial applications.
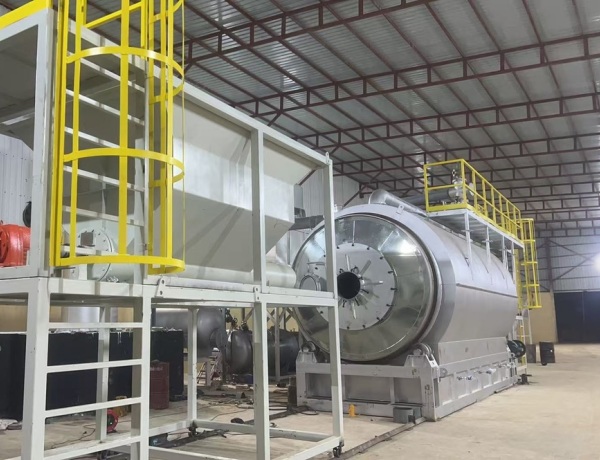
Product Keyword Integration: The Hallmarks of KESMI Continuous Thermal Desorption Units
KESMI’s solutions deliver a competitive edge across multiple product keywords: continuous thermal desorption unit, thermal desorption system, soil remediation machine, hazardous waste treatment equipment, VOCs removal technology, industrial cleanup equipment, contaminated soil treatment plant, organic pollutant removal machinery, environmental restoration equipment, thermal remediation system, solid waste desorption unit, hydrocarbon removal equipment, integrated desorption plant, remediation process automation, continuous feed desorption technology, high-temperature soil treatment plant, industrial waste remediation system, fully automatic thermal desorption facility. Each solution is tailored to tackle complex contamination scenarios while maximizing uptime, throughput, and safety standards.
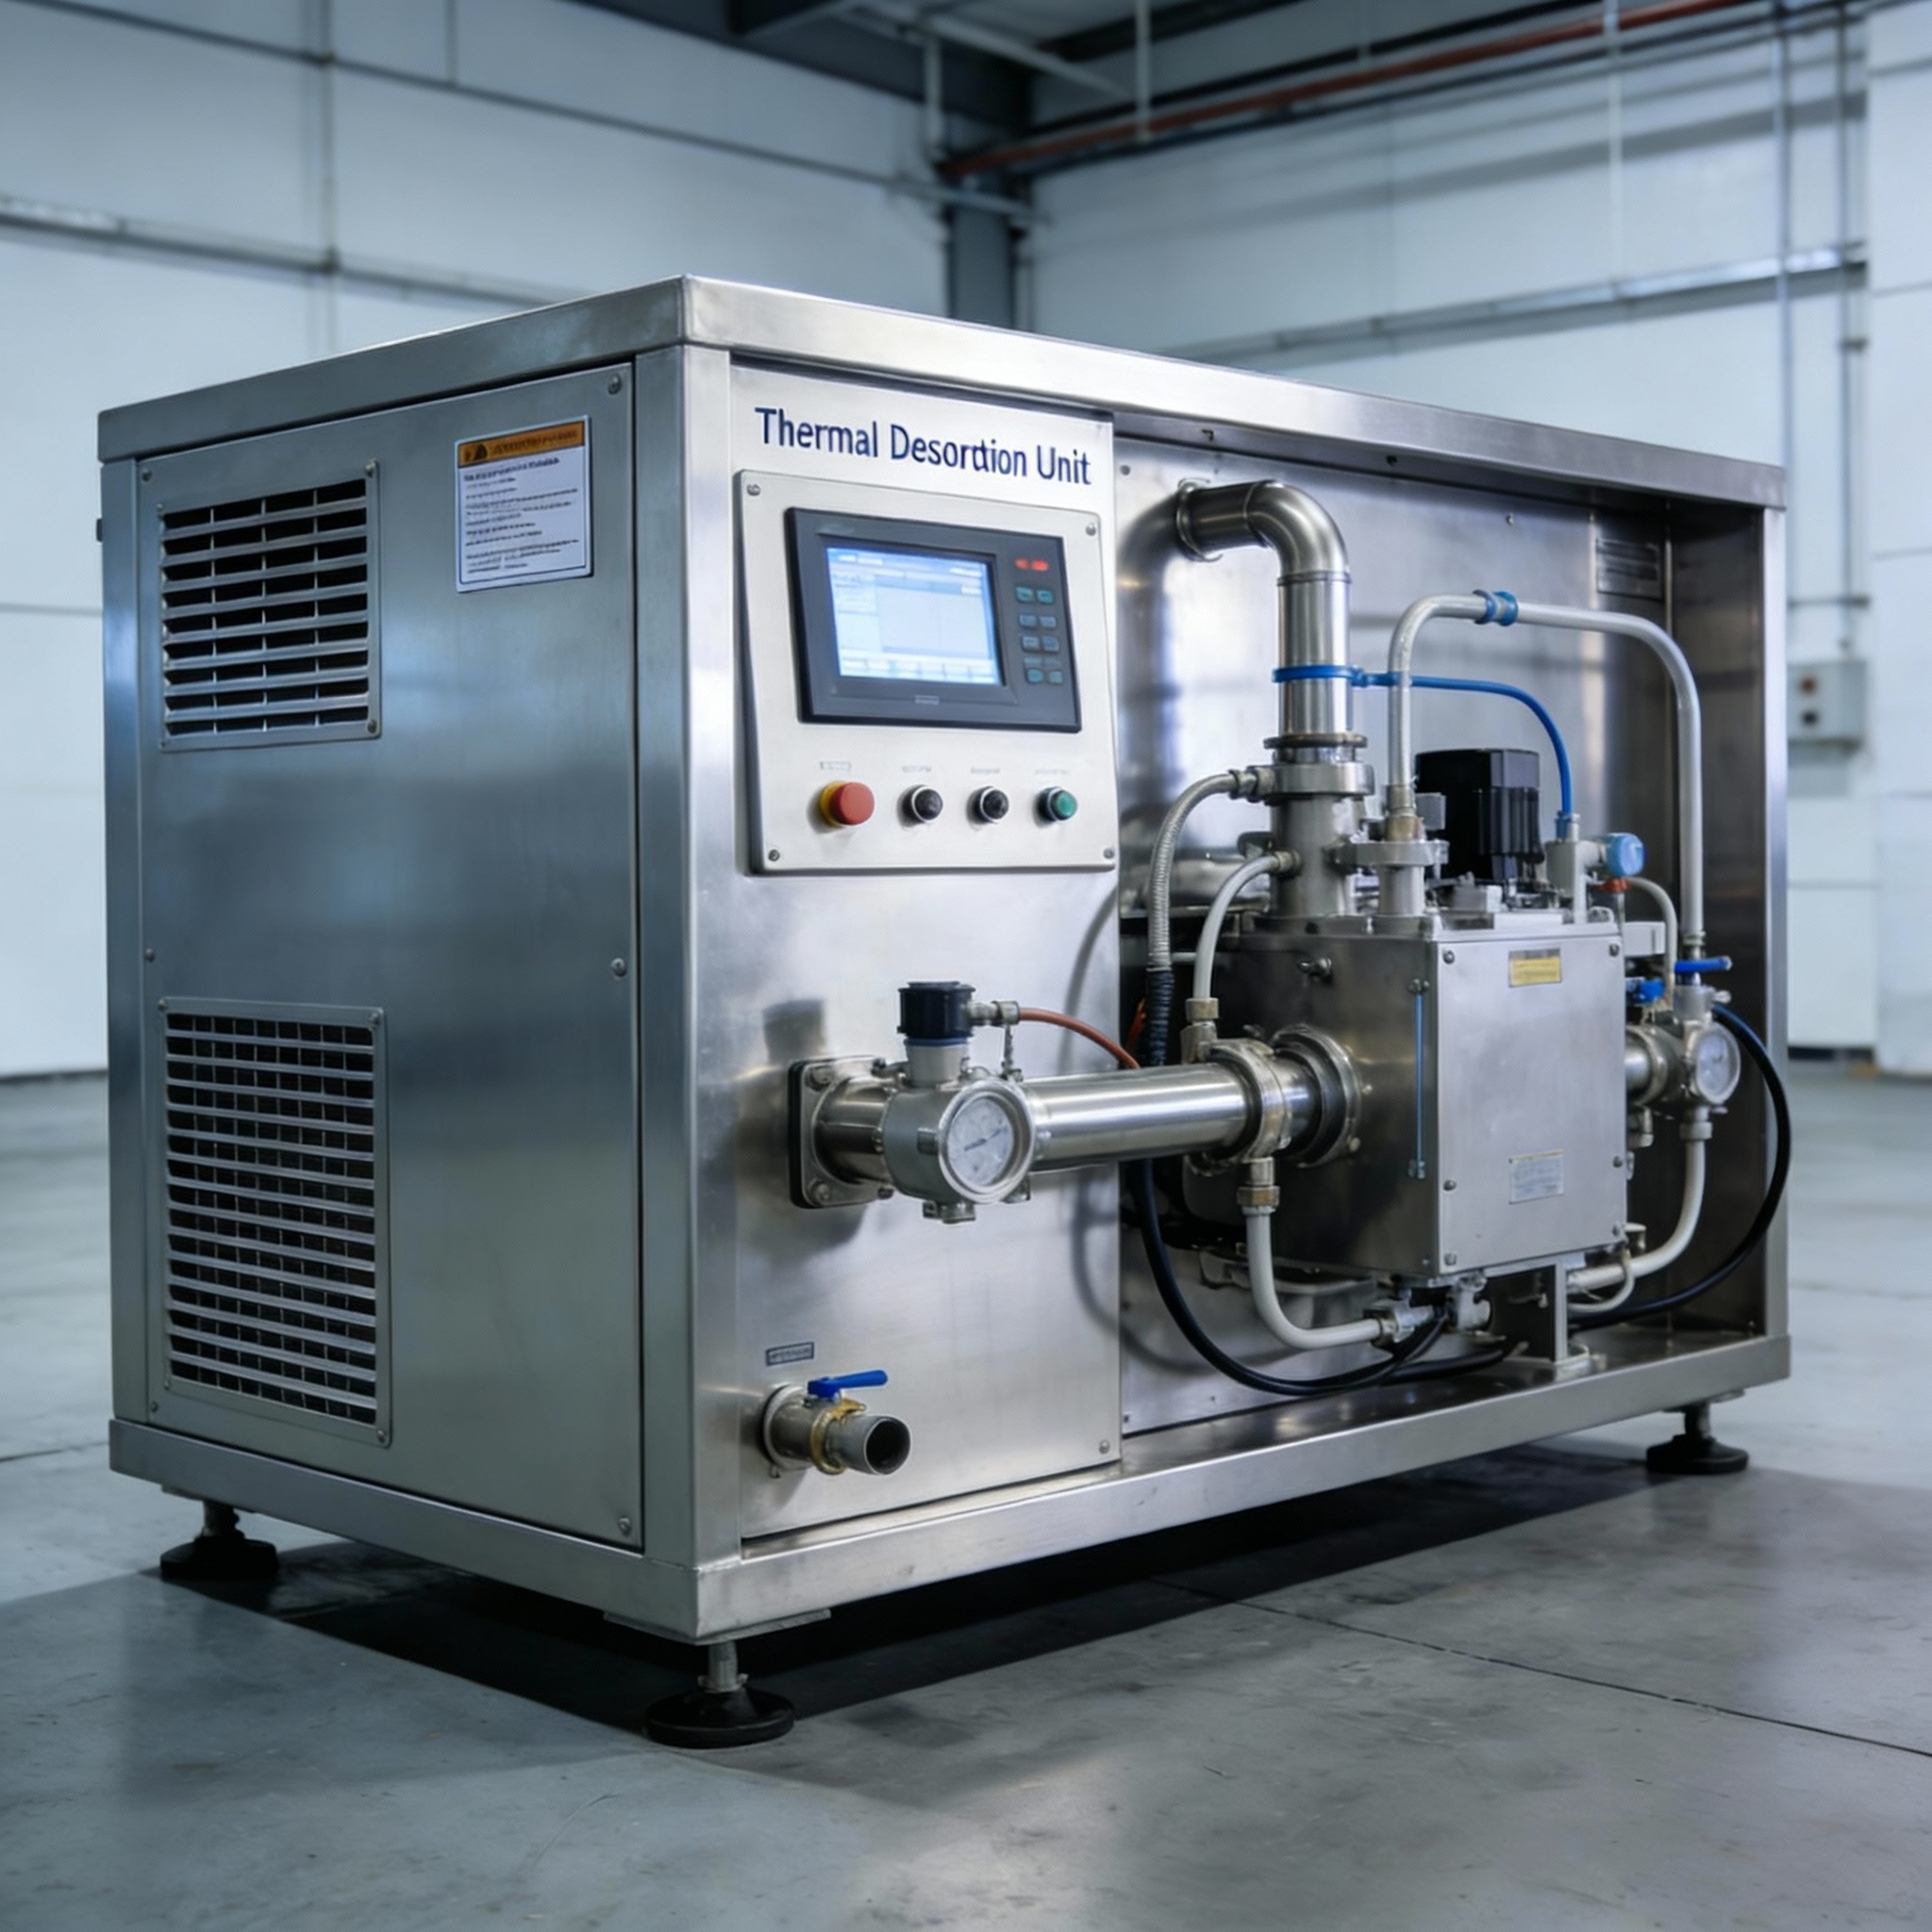
Thermal Desorption Unit
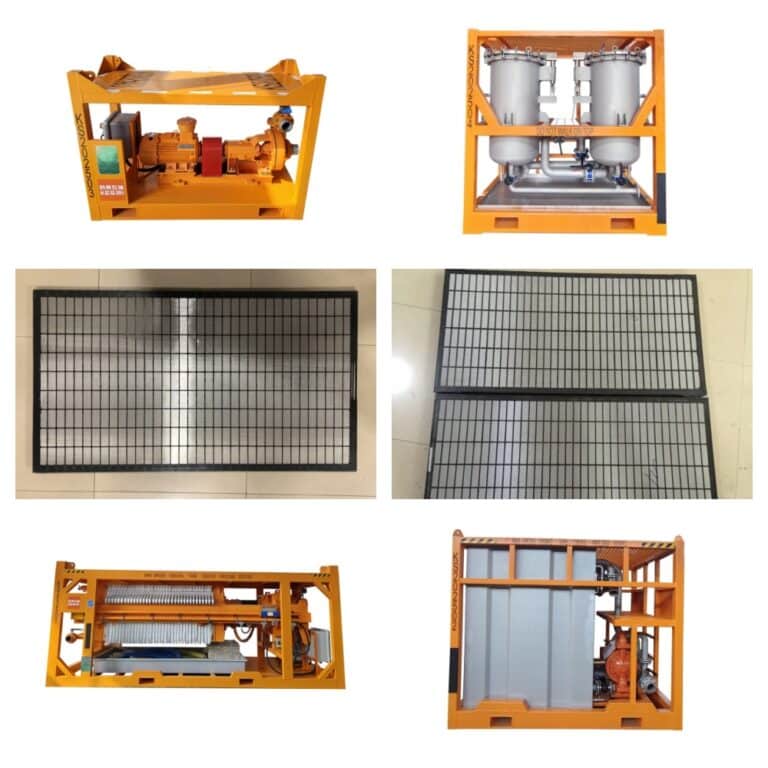
Industrial Package Equipment for Oil field
Understanding Continuous Thermal Desorption Unit Technology
Continuous thermal desorption units fundamentally operate by heating contaminated media (such as soil or sludge) to temperatures that volatilize and separate hazardous organic compounds. KESMI’s CTDU technology ensures a seamless, automated process with precise temperature control and rapid throughput, critical for high-volume industrial cleanup projects. The integration of advanced sensors and control systems allows for real-time monitoring and process adjustment, minimizing energy consumption and maintaining consistent results.
The main benefits include:
- Efficient organic pollutant removal
- Reduced environmental liability
- Compliance with global remediation standards
- Minimized operational downtime
- Scalable solutions for projects of any size
Innovative Features: KESMI’s Competitive Advantage
KESMI CTDU solutions are distinguished by their modular design, robust construction, and intelligent process automation. Key innovations include:
- Continuous feed desorption technology for uninterrupted operation
- High-temperature soil treatment with adaptable heating profiles
- Integrated emission controls for VOCs removal and air quality management
- Real-time process data acquisition and remote monitoring capabilities
- Flexible plant layouts for rapid deployment and relocation
- Energy-efficient design, reducing operational costs and carbon footprint
Application Scope: Addressing the Full Spectrum of Industrial Cleanup Needs
KESMI’s continuous thermal desorption units are widely deployed in:
- Soil remediation for oil spills and hydrocarbon contamination
- Hazardous waste treatment at industrial manufacturing sites
- Environmental restoration projects for brownfield redevelopment
- Industrial waste remediation in petrochemical, mining, and pharmaceutical sectors
- VOCs removal for air quality compliance
- Solid waste desorption for landfill reclamation and safe disposal
Purchasing Psychology: Why Leading Buyers Choose KESMI
As experienced buyers and technical specialists, your priorities are clear: reliability, performance, compliance, and total cost of ownership. KESMI delivers on these fronts by offering fully automatic thermal desorption facilities that require minimal operator intervention, reducing labor costs and risk. Our established track record provides assurance of robust after-sales support, spare part availability, and technical consulting, setting KESMI apart from generic suppliers.
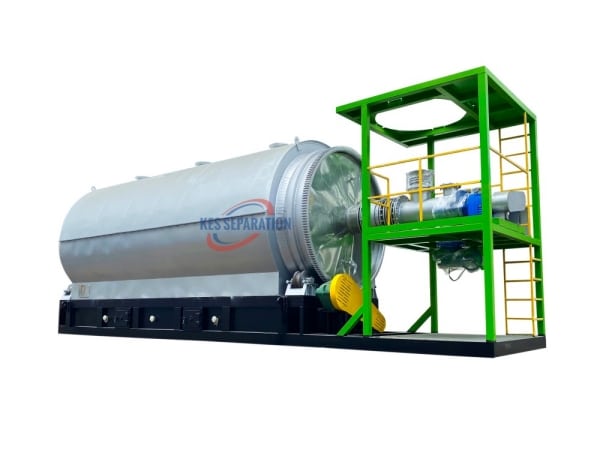
We understand the risks associated with environmental remediation—unexpected downtime, regulatory fines, and safety incidents can undermine project profitability. That’s why KESMI’s remediation process automation and integrated desorption plant solutions focus on operational certainty. With proven industrial cleanup equipment, buyers secure their investment against future liabilities and maintain project schedules.
Technical Expertise: Professional Solutions from China’s Premier Manufacturer
KESMI’s engineering team possesses deep knowledge of the thermal desorption process, from material handling to advanced process control. Our expertise ensures that every contaminated soil treatment plant and hydrocarbon removal equipment package is custom-configured to fit site-specific conditions, contamination profiles, and throughput requirements.
We support buyers through every stage, including:
- Feasibility study and technical assessment
- System design and plant layout optimization
- Installation, commissioning, and operator training
- Post-installation performance audits
- Remote troubleshooting and process upgrades
Global Compliance and Proven Results
KESMI’s thermal remediation systems are built to meet stringent international standards, including EPA, EU, and Chinese environmental regulations. Our contaminated soil treatment plants have been successfully deployed across Asia, Europe, the Middle East, and Africa, supporting multinational clients in achieving regulatory compliance and environmental restoration goals.
Integrated Solutions: From Standalone Units to Turnkey Environmental Restoration Equipment
Our product portfolio spans from compact solid waste desorption units for small-scale operations to fully automatic thermal desorption facilities for continuous industrial waste remediation. KESMI’s integrated desorption plant solutions are designed to adapt to diverse project demands, seamlessly integrating with upstream and downstream processes such as soil excavation, waste handling, and emission management.
VOCs Removal Technology & PLC Control System: Transforming Industrial Cleanup
Two critical keywords for industrial buyers are VOCs removal technology and PLC control system. KESMI integrates advanced VOCs removal modules—including thermal oxidizers and carbon adsorption beds—ensuring emissions are safely managed and compliant with air quality standards. Our PLC control systems automate the entire remediation process, offering precise, programmable control over temperature, feed rate, and emissions management, facilitating remote operation and real-time process optimization. These features are essential for reducing manual intervention, improving accuracy, and ensuring consistent output.
Procurement Perspective: Key Considerations for Industrial Buyers
When specifying a continuous thermal desorption unit, buyers should look beyond just upfront cost. KESMI’s solutions offer:
- Long-term reliability and low maintenance
- Availability of technical support and spare parts
- Customizable design for local regulatory requirements
- Ease of integration with existing site infrastructure
- Flexible financing and global shipping options
Case Studies: Delivering Results for Genuine Buyers
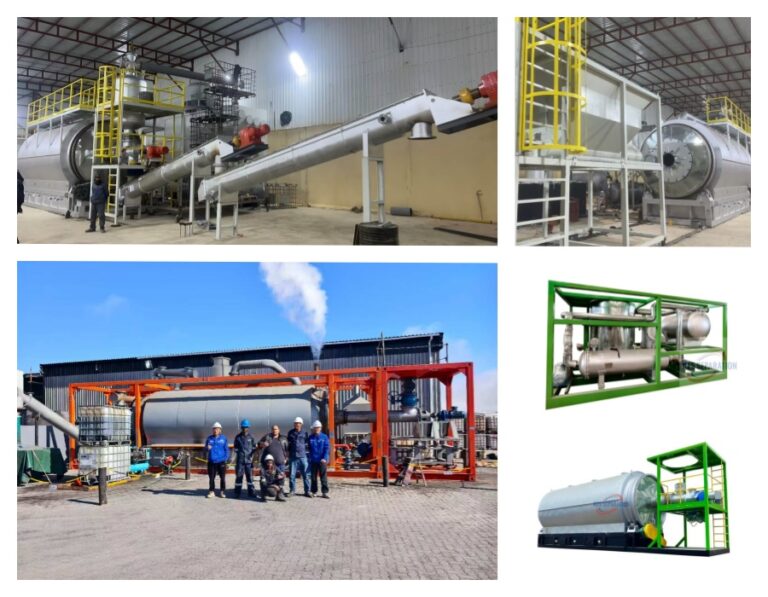
Industrial buyers value real-world proof. KESMI has delivered successful remediation projects for large oil refineries, chemical plants, and contaminated land redevelopment. Clients report rapid ROI, predictable performance, and streamlined regulatory approval thanks to KESMI’s expertise and robust equipment.
After-Sales Service and Customer Support
KESMI’s commitment to buyers does not end at installation. We offer comprehensive after-sales service, spare parts logistics, process optimization consulting, and remote monitoring to ensure your thermal desorption system operates at peak efficiency for years to come.
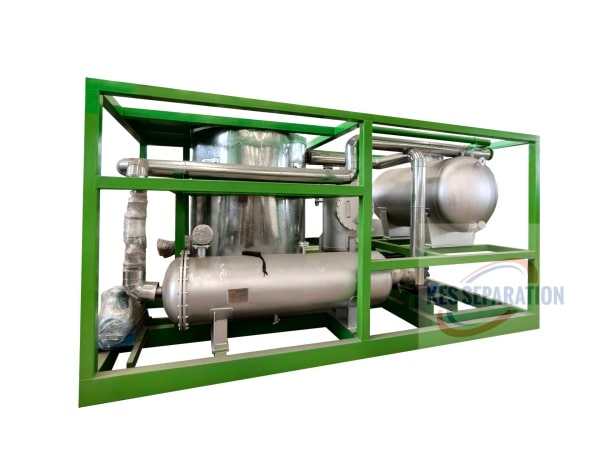
Why KESMI? The Manufacturer’s Perspective
As a manufacturer, KESMI’s philosophy is delivering value beyond machinery. We invest in R&D, maintain strict quality control, and build long-term partnerships with buyers. Our solutions are not just products—they are guaranteed pathways to regulatory compliance, environmental protection, and economic sustainability. This approach resonates with genuine purchasing buyers who seek quality, reliability, and partnership, not just transactional solutions.
Contact KESMI: Turn Your Cleanup Challenges into Success
Ready to advance your industrial cleanup project with proven continuous thermal desorption technology? Contact KESMI for expert consulting and tailored solution recommendations. We are prepared to support genuine buyers in achieving operational excellence, environmental restoration, and regulatory compliance.
Summary Table: Key Advantages of KESMI Continuous Thermal Desorption Units
| Feature | Benefit |
|---|---|
| Continuous Feed Operation | Maximized throughput, reduced labor cost |
| PLC Control System | Automated process, real-time optimization |
| VOCs Removal Technology | Emission compliance, safe air quality |
| Modular Design | Scalable, rapid deployment |
| Integrated Emission Controls | Minimized environmental impact |
| Global Compliance | Streamlined regulatory approval |
| After-Sales Support | Operational reliability, long-term partnership |
Conclusion: KESMI – Trusted Partner for Industrial Cleanup
Industrial buyers seeking reliable, high-performance continuous thermal desorption units for soil remediation, hazardous waste treatment, VOCs removal, and environmental restoration need look no further than KES Separation Machinery Co. Ltd (KESMI). With deep technical expertise, proven track record, and genuine commitment to buyer success, KESMI stands as the partner of choice for transformative industrial cleanup solutions.