How Does Brine Filtration Equipment Manufacturer Optimize Membrane Technology for Superior Performance
KES Separation Machinery Co. Ltd (KESMI) is a leading Chinese manufacturer specializing in optimized brine filtration equipment, advanced membrane technology, and comprehensive brine purification systems. By tailoring membrane selection, integrating advanced pre-treatment, and automating cleaning processes, KESMI delivers high-efficiency solutions for industrial brine filtration, high-salinity water treatment, and seawater desalination. The company’s modular designs enable scalability and easy maintenance, addressing buyers’ demands for reliability, cost reduction, and future-proofing. KESMI’s expertise extends to integrating brine filtration with zero liquid discharge (ZLD) and sludge dewatering equipment, supporting holistic water management for industries like power generation and food processing. With competitive pricing, robust after-sales service, and technical customization, KESMI stands out as the trusted supplier for procurement professionals seeking superior performance and operational excellence.
Introduction: Elevating Brine Filtration Standards with KESMI
In today’s highly competitive industrial landscape, choosing the right Brine filtration equipment manufacturer can determine the success of your process efficiency, product purity, and operational continuity. KES Separation Machinery Co. Ltd, known as KESMI, stands as a reputable brine filtration equipment manufacturer and supplier in China, specializing in the optimization of membrane technology to deliver superior brine filtration systems, industrial brine filtration solutions, and advanced brine purification equipment.
Understanding the Core Needs of Industrial Buyers
Experienced procurement professionals prioritize reliability, cost-efficiency, and technical innovation when selecting brine filtration systems. KESMI responds to these priorities by customizing solutions for sodium chloride brine filtration, high-salinity water treatment, and integrated membrane separation systems. Our expertise addresses common pain points: reducing maintenance costs, achieving consistent product quality, and ensuring environmental compliance.

Product Portfolio Overview: Brine Filtration Equipment & Membrane Solutions
- brine filtration systems
- Industrial Brine Filtration Equipment
- High-Salinity Water Treatment Systems
- Brine Purification Equipment
- Membrane Brine Filtration Units
- Sodium Chloride Brine Filtration Equipment
- Brine Ultrafiltration Membrane Equipment
- Reverse Osmosis Brine Filtration Systems
- Brine Desalination Membrane Modules
- Electrodialysis Brine Concentration Equipment
- Saltwater Filtration Membrane Systems
- Brine Clarification Systems
- Seawater Desalination Membrane Equipment
Key Optimization Strategies for KESMI Membrane Technology
1. Precision Membrane Selection and Customization
KESMI employs a diverse range of high-performance ultrafiltration, nanofiltration, and reverse osmosis membranes. By matching specific membrane materials and pore sizes to your brine’s composition, we ensure high flux rates, reduced fouling, and maximum contaminant removal. Our sodium chloride brine filtration equipment and brine ultrafiltration membrane equipment are widely used in chlor-alkali, food processing, and chemical manufacturing industries.
2. Advanced Pre-Treatment Integration
Pre-filtration and pre-treatment are critical for extending membrane lifespan. KESMI integrates automatic self-cleaning filters and advanced chemical dosing units ahead of membrane modules, minimizing scaling and organic fouling. This pre-treatment step is especially crucial for high-salinity water treatment systems and seawater desalination membrane equipment—ensuring stable and long-term operation.
3. Automated Membrane Cleaning and Regeneration
Our brine filtration systems feature programmable Clean-In-Place (CIP) modules and real-time monitoring sensors. These enable predictive maintenance and scheduled cleaning cycles tailored to your process. KESMI’s brine purification equipment minimizes downtime, enhances total cost of ownership, and guarantees consistent filtrate quality for critical applications.
4. Modular Design for Scalability and Serviceability
KESMI brine filtration equipment is engineered for modularity, supporting rapid capacity expansion and minimal intervention during upgrades or repairs. This design philosophy is highly valued by procurement teams seeking flexible, future-proof solutions for evolving industrial demands, including brine clarification systems and brine desalination membrane modules.
Performance Advantages: Why KESMI Stands Out
- High Rejection Rates: Our reverse osmosis brine filtration systems consistently achieve salt rejection rates above 99.5% and minimize hardness, heavy metals, and organic contaminants.
- Energy Efficiency: Innovative membrane formulations and energy recovery systems reduce operational costs—critical for large-scale saltwater filtration membrane systems.
- Longevity and Reliability: Superior anti-fouling coatings and robust module housings extend equipment lifespan, reducing replacement frequency and lifecycle costs.
- Regulatory Compliance: KESMI brine filtration equipment meets stringent global standards (e.g., ISO, CE), ensuring safe integration into regulated industries.
- Customization Capability: Our technical team collaborates with clients to tailor equipment—whether for electrodialysis brine concentration equipment or niche sodium chloride brine filtration requirements.
Integrating Brine Filtration with Zero Liquid Discharge (ZLD) and Sludge Dewatering Equipment
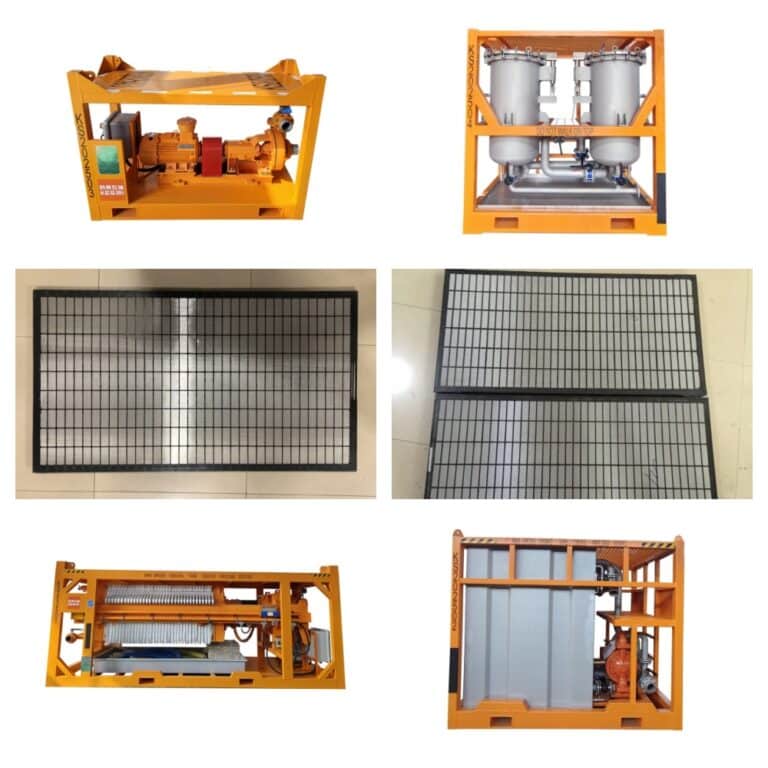
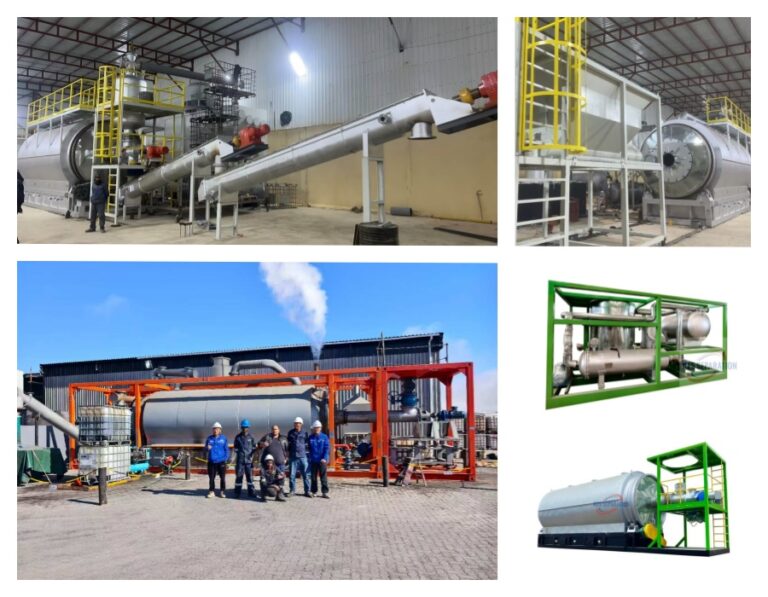
As industrial buyers seek holistic waste management solutions, KESMI offers seamless integration of brine filtration systems with zero liquid discharge (ZLD) process modules. This strategic approach achieves maximum water recovery and minimizes environmental impact. Additionally, pairing with our advanced sludge dewatering equipment ensures efficient handling of residual solids, streamlining the entire water treatment workflow for industries such as power generation, mining, and food processing.
Comprehensive After-Sales Support and Global Service
Our commitment extends beyond equipment delivery. KESMI provides remote diagnostics, on-site commissioning, operator training, and rapid spare parts supply. With an international footprint and a responsive technical team, KESMI guarantees continuous support for all brine filtration equipment, including membrane brine filtration units and brine purification systems worldwide.

Why Procurement Professionals Choose KESMI as Their Trusted Brine Filtration Equipment Supplier
- Direct factory pricing and flexible payment options
- Proven industrial references and case studies
- Fast turnaround for project customization and delivery
- Comprehensive technical documentation for seamless integration
Conclusion: Invest in Future-Ready Brine Filtration Solutions with KESMI
KES Separation Machinery Co. Ltd (KESMI) empowers industrial buyers with advanced, optimized brine filtration equipment solutions, leveraging state-of-the-art membrane technology. Our focus on product innovation, reliability, and end-to-end customer support makes us the preferred supplier for demanding applications worldwide. Contact KESMI today to discuss your brine filtration, zero liquid discharge, and sludge dewatering equipment needs—and transform your operational efficiency with confidence.