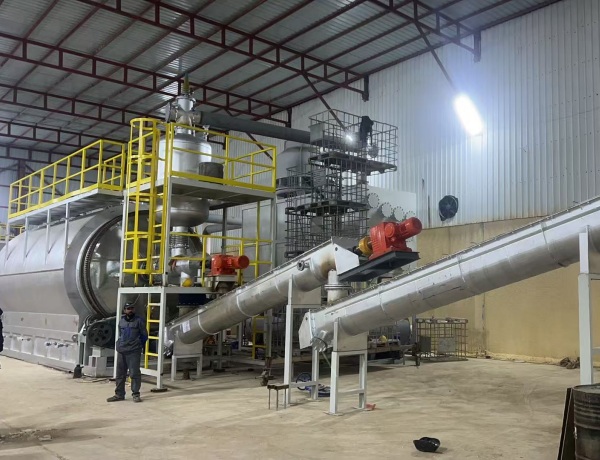
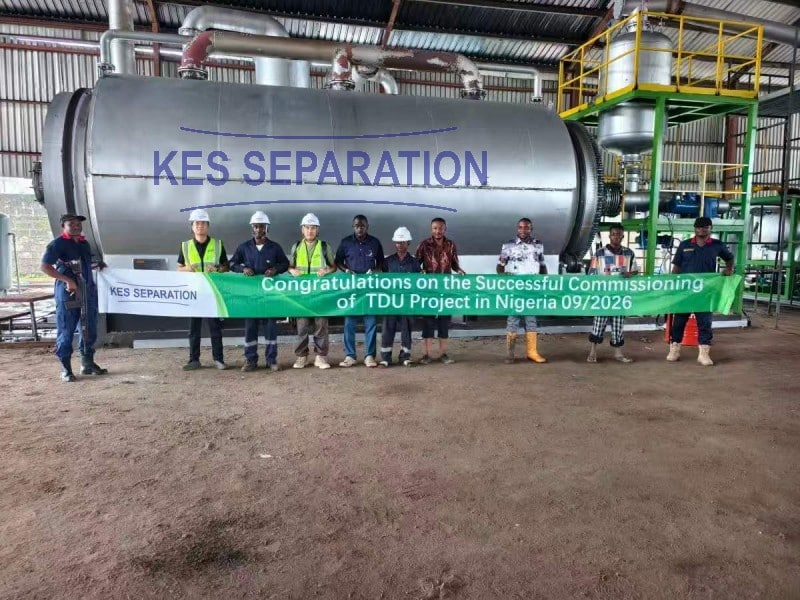
In September 2026, a Thermal Desorption Unit (TDU) supplied by KES Separation was successfully installed, commissioned and trial-operated at a project site in Nigeria.
Following equipment inspection, mechanical adjustment, system connection and operation testing, the TDU successfully completed the commissioning stage and has now entered the subsequent operation phase.
From Equipment Installation to Commissioning
For thermal desorption applications, equipment operation is closely related to feedstock characteristics, feeding method, site conditions and on‑site operating practices.
For this reason, the KES technical team closely monitored the real‑time operating status of the TDU throughout commissioning. Site‑based local personnel took part in inspection and operational procedures. Through hands‑on practice, local operators gained solid familiarity with core workflows, including feeding, heating, rotary running, material discharge and system shutdown.
For overseas projects, such close communication between KES technical engineers and local operators constitutes a vital part of commissioning. It enables on‑site staff to fully comprehend the equipment, and lays a practical foundation for future daily operation and maintenance.
On-Site Operation Testing
After installation and necessary adjustments were completed, the TDU was put through on-site operation testing.
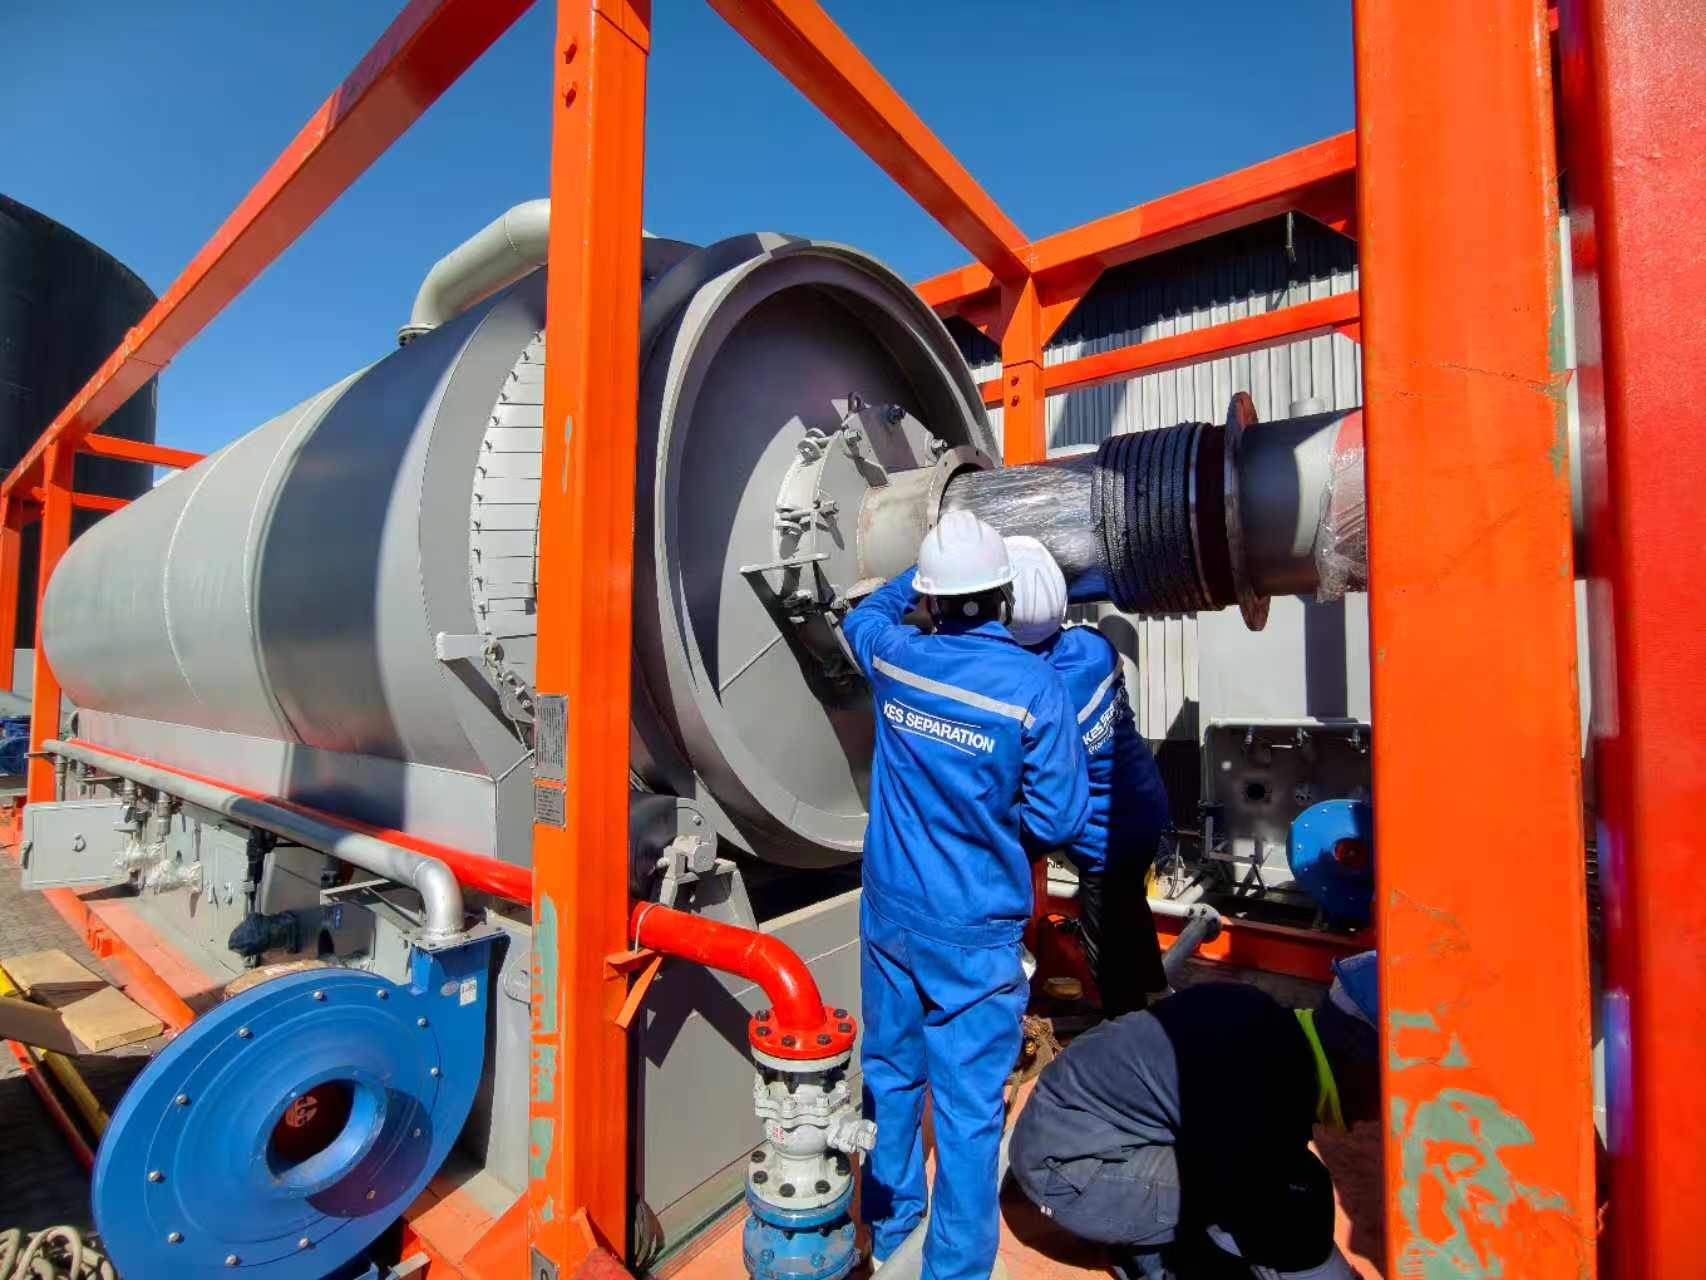
During the testing process, KES team checked the operating condition of the rotary system, drive components, feeding and discharge sections, as well as the relevant piping connections. The team also paid attention to equipment vibration, connection conditions and the coordination between different mechanical components during operation.
As shown in the project photos, the site personnel were carrying out mechanical inspection and adjustment work around the feeding section of the TDU. Local operators also worked together with KES team during the commissioning process.
Turning Oil-Containing Waste into Recoverable Resources
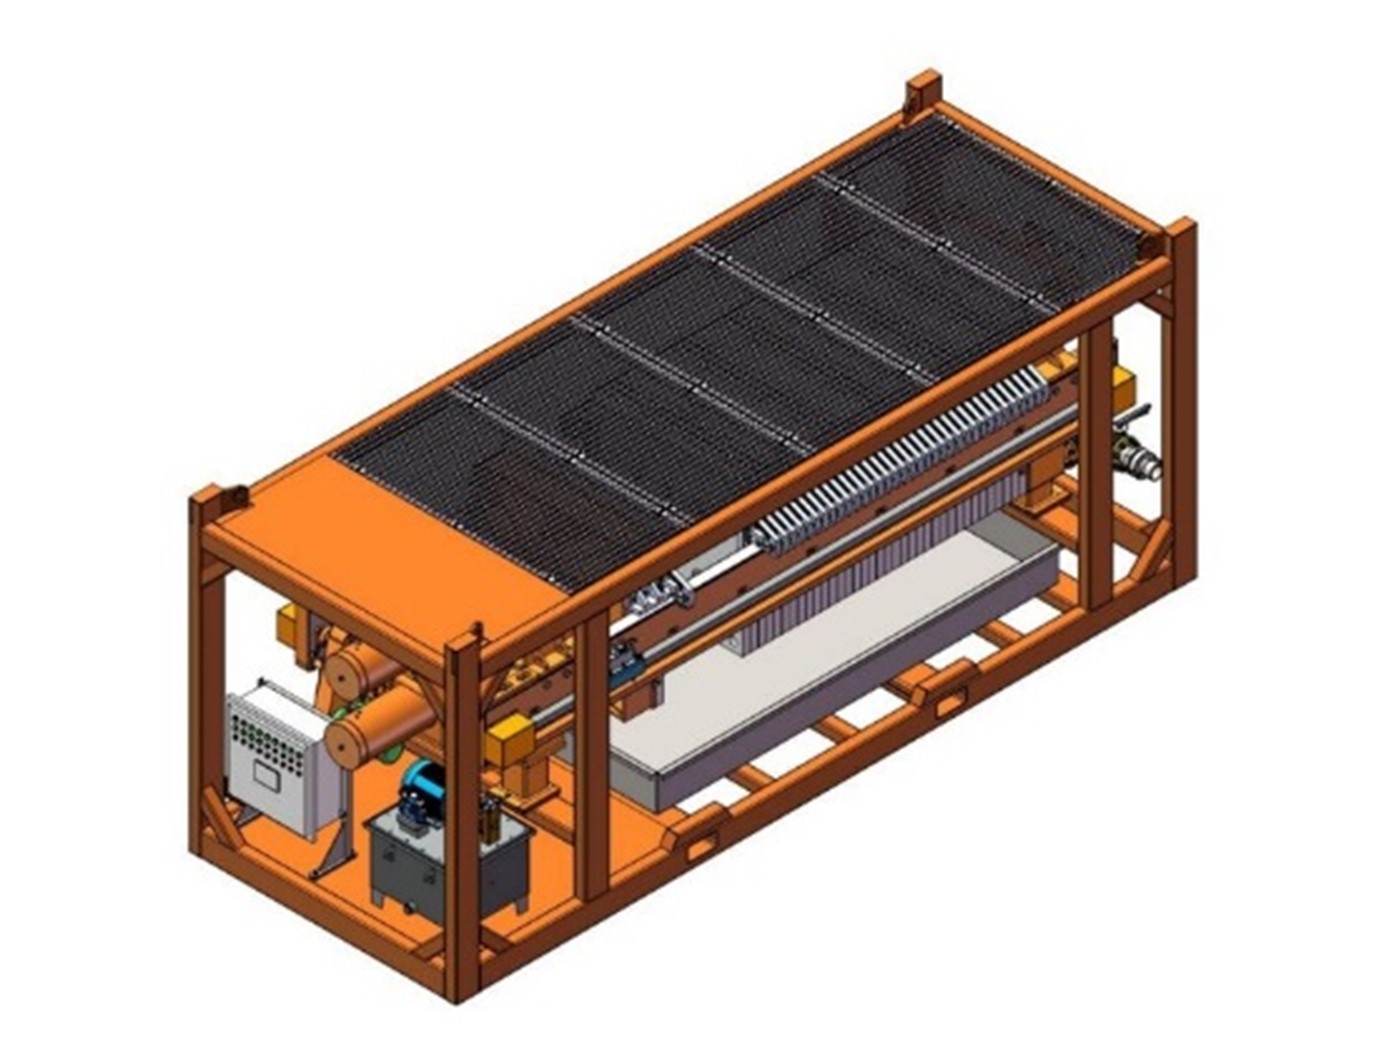
This thermal desorption system is purpose‑built for harmless and resource‑oriented disposal of oil‑bearing solid waste generated from oil‑and‑gas operations, including oily sludge, oil‑based drilling cuttings and hydrocarbon‑contaminated soil. With proven indirect high‑temperature thermal desorption technology, materials are thermally pyrolysed under sealed oxygen‑free conditions. Most hydrocarbon components are separated and recovered as reusable oil products. After treatment, the oil content of solid residues meets local environmental regulatory standards. The solution delivers triple value: waste volume reduction, pollutant detoxification and oil‑resource recovery, providing critical technical support for local environmental governance of Nigeria’s oil & gas industry.
Successful Completion of the Nigeria Project
The successful commissioning of this TDU project marks another field application of KES Separation thermal desorption technology in Nigeria.
Throughout the project, KES focused not only on equipment manufacturing and delivery, but also on the installation, commissioning and operation support after the equipment arrived at the site.
As the TDU moves into the subsequent operation stage, KES will continue to provide necessary technical support and follow the unit’s operating performance based on actual site conditions and operating data.
The project also provides KES with further practical experience for thermal desorption and drilling waste treatment applications in Nigeria and the wider West African market.
From equipment manufacturing and delivery to on-site installation, commissioning and technical support, KES will continue to work closely with customers and develop equipment solutions based on actual project requirements.